


Pumps for Chemical Processing
Reliable, safe, and efficient chemical pump solutions for demanding industrial applications.
The chemical industry places extreme demands on rotating equipment. Pumps must withstand aggressive chemicals, extreme temperatures and high pressures while maintaining safety and efficiency. Failure to properly maintain pumps can lead to leaks, downtime and environmental hazards.
At AVTPUMP, we specialise in servicing, repairing and optimising chemical pumps to keep your plant running safely and efficiently. Through expert root cause analysis, component upgrades and condition monitoring, we enhance performance, extend asset life and reduce the risk of failure.
- Enhanced safety for plant personnel and the environment
- Increased pump efficiency and reliability
- Reduced mean time between failures (MTBF)
- Lower maintenance and operational costs
- Independent, manufacturer-agnostic advice focused on best-fit solutions
- Support for all pump makes and models, not limited to a single OEM
- Fast response for critical repairs and minimised downtime
- Lifecycle approach, from repair and upgrade through to monitoring and optimisation
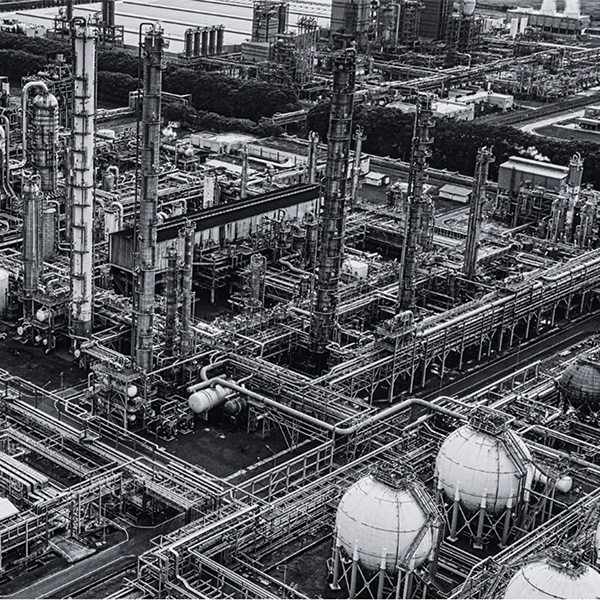
The chemical industry places extreme demands on rotating equipment. Pumps must withstand aggressive chemicals, extreme temperatures and high pressures while maintaining safety and efficiency. Failure to properly maintain pumps can lead to leaks, downtime and environmental hazards.
At AVTPUMP, we specialise in servicing, repairing and optimising chemical pumps to keep your plant running safely and efficiently. Through expert root cause analysis, component upgrades and condition monitoring, we enhance performance, extend asset life and reduce the risk of failure.
Safety: Enhanced safety for plant personnel and the environment.
Reliability: Increased pump efficiency and reliability.
Reduced failure rates: Reduced mean time between failures (MTBF).
Lower costs: Lower maintenance and operational costs.
Independent advice: Manufacturer-agnostic support focused on best-fit solutions.
All makes and models: Support across pump types, not limited to a single OEM.
Fast response: Critical repair support to minimise downtime.
Lifecycle approach: From repair and upgrade through to monitoring and optimisation.
Benefits of Regular Servicing and Upgrades
Proactive maintenance and targeted upgrades can significantly improve pump reliability, reduce costs and safeguard your chemical processing environment.
Enhanced safety
Support safer operation for plant personnel and the environment.
Improved reliability
Increase pump efficiency and support dependable performance.
Fewer failures
Reduce mean time between failures (MTBF) through proactive support.
Lower operating costs
Reduce maintenance demands and long-term operational costs.
Benefits of Regular Servicing and Upgrades
Proactive maintenance and targeted upgrades can significantly improve pump reliability, reduce costs and safeguard your chemical processing environment.
Enhanced safety: Support safer operation for plant personnel and the environment.
Improved reliability: Increase pump efficiency and support dependable performance.
Fewer failures: Reduce mean time between failures (MTBF) through proactive support.
Lower operating costs: Reduce maintenance demands and long-term operational costs.
Common Problems with Chemical Pumps, and How AVTPUMP Solves Them
Corrosion & Erosion
Aggressive chemicals degrade pump components over time.
Solution: Material upgrades, protective coatings and sealing solutions to extend lifespan.
Seal Failures & Leaks
Hazardous leaks jeopardise safety and compliance.
Solution: Advanced sealing technologies including IP69K bearing protection and double mechanical seals.
Cavitation & Efficiency Loss
Cavitation can reduce efficiency, accelerate wear and shorten component and system life.
Solution: Performance reviews and predictive monitoring to prevent failures and improve efficiency.
Trusted Manufacturers for Chemical Pumps
Klaus Union
Specialists in magnetic drive pumps for hazardous environments.

KSB Pumps
High-performance chemical pump solutions for aggressive fluids.

Chemquip Pumps
Providers of chemical-specific pumping systems with corrosion resistance.