Ageing Assets
Maintaining Critical Production Through Modernisation and Compatibility
Chemical Processing Download Case Study (PDF)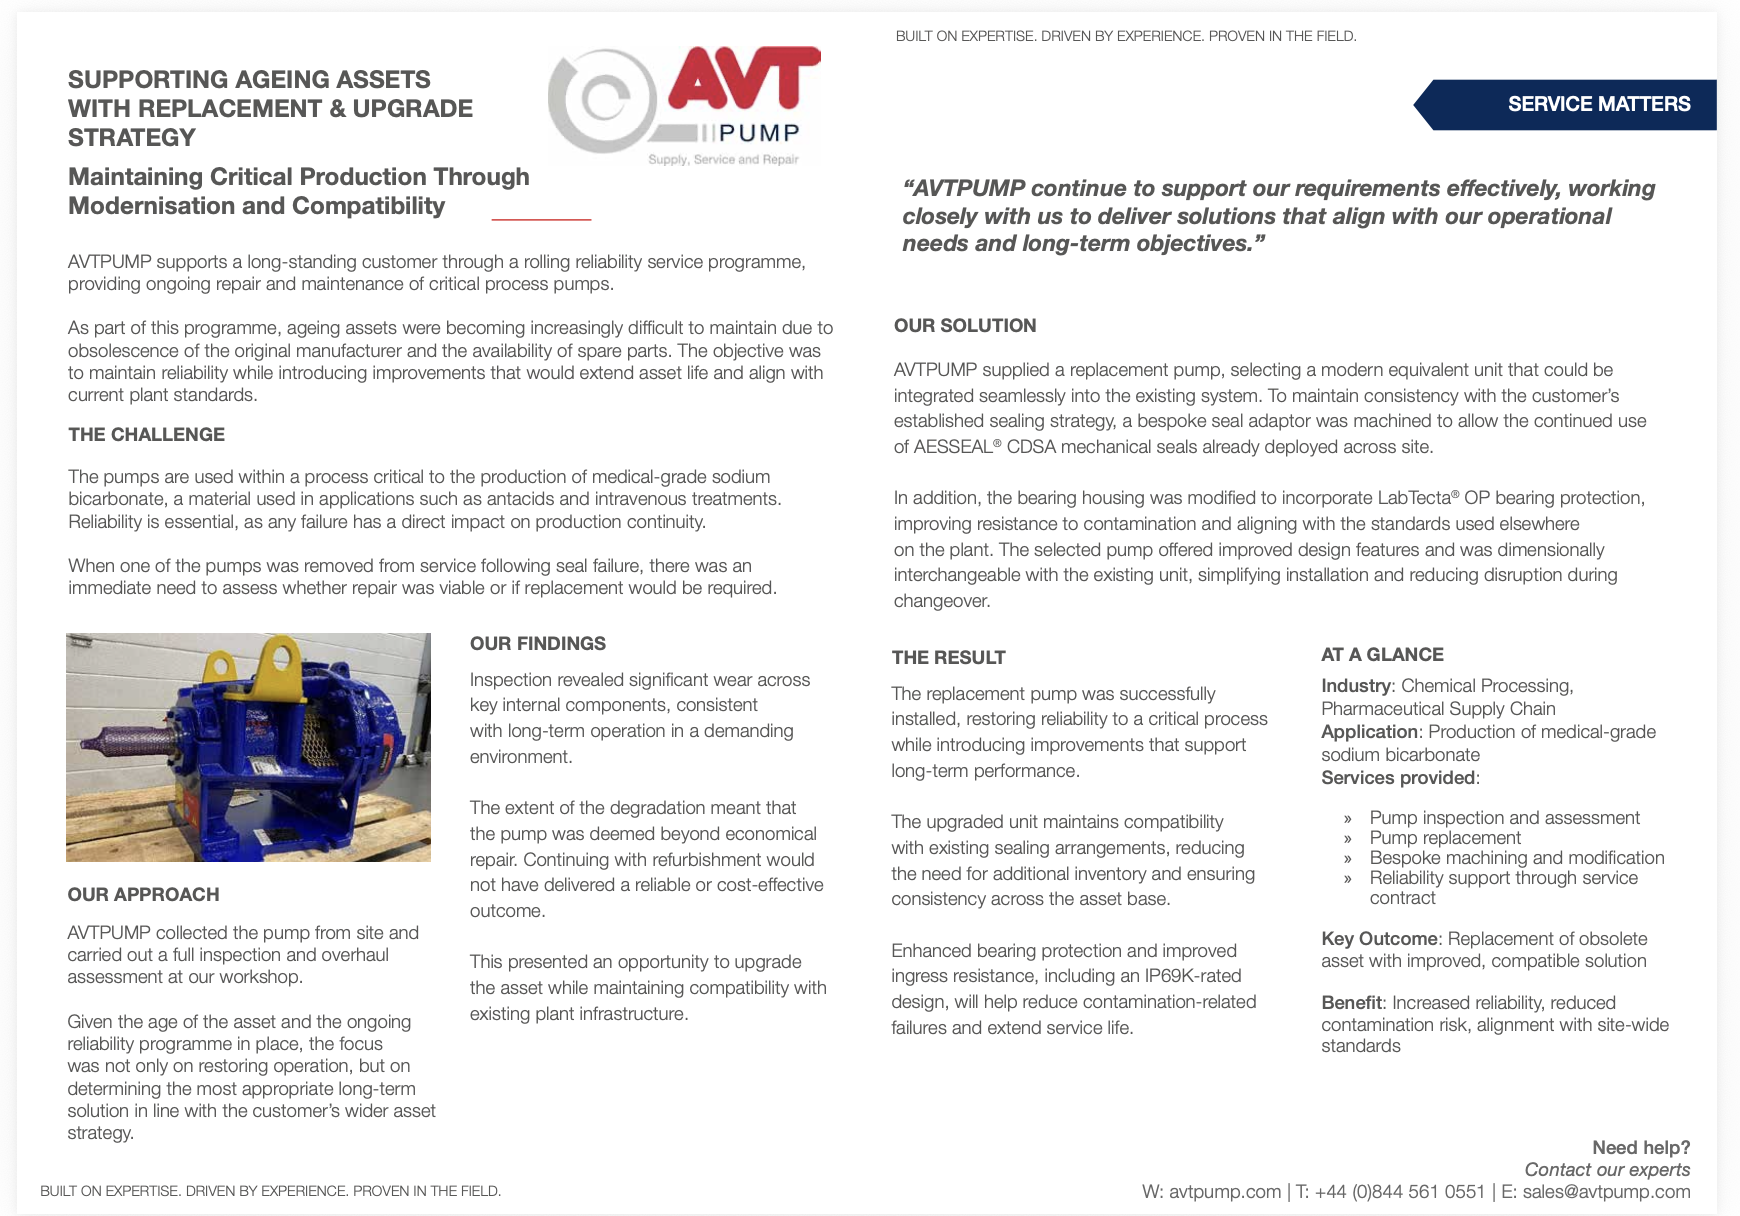
Working to Achieve
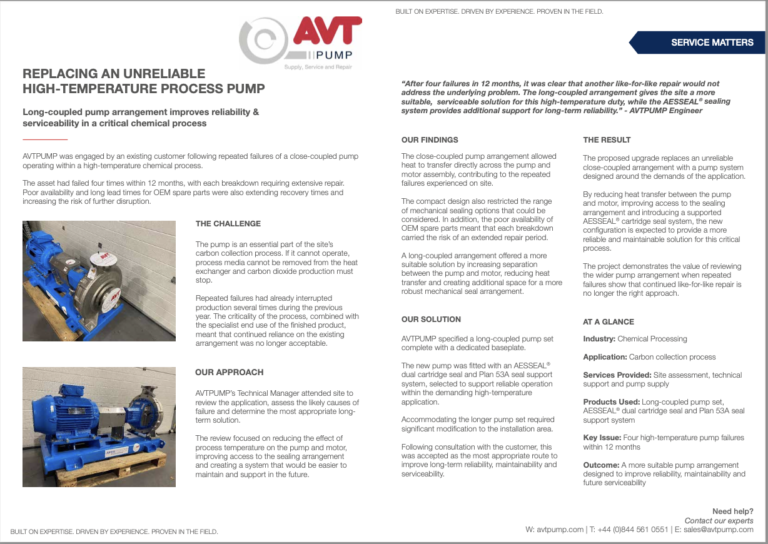
AVTPUMP supports a long-standing customer through a rolling reliability service programme, providing ongoing repair and maintenance of critical process pumps. As part of this programme, ageing assets were becoming increasingly difficult to maintain due to obsolescence of the original manufacturer and the availability of spare parts. The objective was to maintain reliability while introducing improvements that would extend asset life and align with current plant standards.
The Challenge
The pumps are used within a process critical to the production of medical-grade sodium bicarbonate, a material used in applications such as antacids and intravenous treatments. Reliability is essential, as any failure has a direct impact on production continuity. When one of the pumps was removed from service following seal failure, there was an immediate need to assess whether repair was viable or if replacement would be required.
Our Findings
Inspection revealed significant wear across key internal components, consistent with long-term operation in a demanding environment. The extent of the degradation meant that the pump was deemed beyond economical repair. Continuing with refurbishment would not have delivered a reliable or cost-effective outcome. This presented an opportunity to upgrade the asset while maintaining compatibility with existing plant infrastructure.
Our Approach
AVTPUMP collected the pump from site and carried out a full inspection and overhaul assessment at our workshop. Given the age of the asset and the ongoing reliability programme in place, the focus was not only on restoring operation, but on determining the most appropriate long-term solution in line with the customer’s wider asset strategy.
The Solution
AVTPUMP supplied a replacement pump, selecting a modern equivalent unit that could be integrated seamlessly into the existing system. To maintain consistency with the customer’s established sealing strategy, a bespoke seal adaptor was machined to allow the continued use of AESSEAL® CDSA mechanical seals already deployed across site. In addition, the bearing housing was modified to incorporate LabTecta® OP bearing protection, improving resistance to contamination and aligning with the standards used elsewhere on the plant. The selected pump offered improved design features and was dimensionally interchangeable with the existing unit, simplifying installation and reducing disruption during changeover.
Follow-Up
The replacement pump was successfully installed, restoring reliability to a critical process while introducing improvements that support long-term performance. The upgraded unit maintains compatibility with existing sealing arrangements, reducing the need for additional inventory and ensuring consistency across the asset base. Enhanced bearing protection and improved ingress resistance, including an IP69K-rated design, will help reduce contamination-related failures and extend service life.
"AVTPUMP continue to support our requirements effectively, working closely with us to deliver solutions that align with our operational needs and long-term objectives."